8m³/H Containerized Reverse Osmosis System | Mobile Industrial Water Purification Plant
Product Introduction
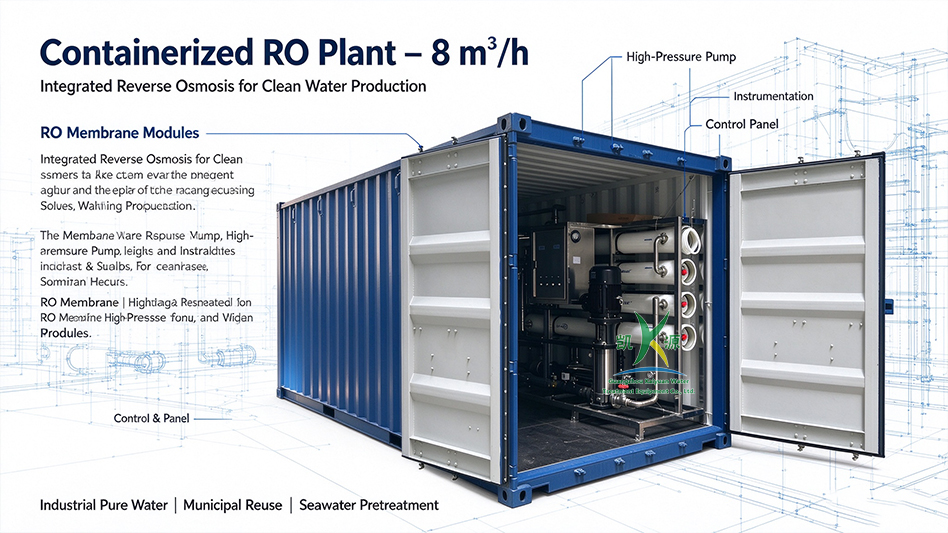
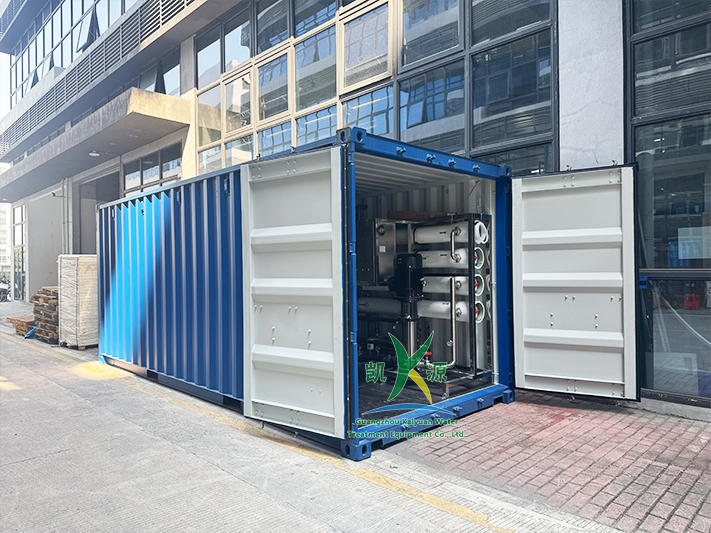
The 8m³/h containerized reverse osmosis system is an integrated, movable water purification equipment developed by our factory for on-site industrial water treatment and engineering projects. It integrates reverse osmosis membrane separation system, multi-stage pretreatment, high-pressure pump set, PLC electrical control cabinet, pipelines, gauges and valve components inside a standard shipping container, forming a compact modular water production unit.
Designed with the core concept of small footprint, rapid deployment and convenient relocation, this unit solves the common pain points of traditional civil-built water stations: long construction period, fixed location limitation and difficult disassembly & relocation. Clients can obtain a small pure water factory packed inside a shipping container, which can be lifted, transported and put into operation at different sites quickly.
All internal assembly, pipeline pressure testing and full machine linkage commissioning are completed before delivery. After arrival at the project site, you only need to connect the inlet/outlet water pipeline and industrial power supply, then stable qualified process pure water can be produced immediately, realizing truly plug-and-play operation.
This RO system can run independently. It can also be used as the front process of secondary RO, EDI or mixed bed water treatment technology, flexibly integrated into industrial production chains with different water quality requirements. Widely adopted for mobile water supply, emergency water supply, overseas engineering projects and decentralized raw water treatment.
Product Nature
- Form Property: Integrated container packaging. The whole system combines pretreatment, membrane system, control unit and pipework inside standard container. It belongs to complete, movable and modular engineering water treatment equipment.
- Process Property: Adopts Reverse Osmosis (RO) as core desalination technology. It is a pressure-driven membrane separation technology. The semipermeable membrane intercepts dissolved ions, colloid, organic matter and microorganisms to realize deep water purification with high salt rejection rate.
- Water Output Property: Produced water includes industrial softened water, process pure water, boiler feed water, recycled wastewater and brackish water desalinated water. Membrane arrangement and water recovery rate can be adjusted according to raw water conditions and water usage requirements.
- Operation Property: Fully automatic continuous operation, low requirement for on-site attendance. The container box has anti-corrosion and weatherproof protection, suitable for outdoor, coastal, mining and oilfield harsh working conditions.
Technical Parameters
Rated Water Production Capacity: 8 m³/h (8 tons per hour)
| Rated permeate flow | 8 m³/h |
| RO membrane element | Industrial 8040 membrane modules, customized by raw water quality |
| Inlet raw water source | Municipal tap water, well water, recycled water, etc. |
| System salt rejection rate | ≥97%~99% (Depends on inlet water and membrane configuration) |
| Water recovery rate | 50%~75% in normal design, adjustable for special projects |
| Working pressure | Controlled by high-pressure pump, automatically adjusted along with membrane pressure drop |
| Control mode | PLC automatic control + touch screen HMI |
| Integration style | Full assembly inside standard container, including pretreatment, pump set, electric system and pipework |
| Power supply | 3-phase industrial power, full integrated electric cabinet |
| Material & protection | Anti-corrosion container housing, 304 stainless steel pipes & industrial fittings |
Note: The above data are typical reference specifications. Final parameters will be confirmed based on raw water quality report and customized process design.
Application Fields
Main Industries & Water Usage Scenarios
- Industrial process water: Pure water preparation for electronics, optics and precision manufacturing industries.
- Boiler & thermal power system: Feed water desalination and softening for steam boilers and power plants.
- Reclaimed water & wastewater reuse: Deep treatment for industrial circulating cooling water and waste water recycling.
- Brackish water & polluted raw water: Brackish water desalination, high-salinity groundwater treatment, municipal recycled water upgrading.
- Food & beverage industry: Process water purification for food processing, beverage blending and brewing.
- Chemical & pharmaceutical pre-treatment: Water for chemical batching and pre-purification for pharmaceutical water system.
- Overseas & field engineering: On-site water supply for oil refining, mining and remote field camps without fixed water plant.
- Emergency & temporary water supply: Short-term water treatment for temporary construction sites, disaster relief and project demonstration.
Product Application Purpose
- Produce industrial pure water: Purify tap water / well water into desalted water that meets production process standards.
- Hardness reduction & softening: Remove calcium and magnesium ions to prevent scaling inside boilers, heat exchangers and pipelines, extend service life of equipment.
- Desalination & ion removal: Reduce TDS and dissolved ions significantly to meet high-standard water quality indexes.
- Reclaimed water upgrading: Deeply purify industrial wastewater for recycling in production lines to save water cost.
- Brackish water desalination: Convert high-salinity raw water into usable fresh water to solve water shortage problems.
- Reusable mobile water supply: As movable water production unit, transfer among different projects to maximize asset utilization rate.
Product Features
- Integrated design & small footprint: Pretreatment, membrane rack, pump set, electric control and pipelines are all installed inside container. Only one crane is needed for placement, no need for civil water tanks or dedicated machine room.
- Plug and play, fast commissioning: Complete assembly and linkage test finished in factory before shipment. Connect power and water pipeline on site to generate purified water, greatly shorten project delivery cycle.
- Easy relocation & multi-scenario use: The whole container can be hoisted and transported. After finishing one project, it can be moved to next site for reuse, improving equipment utilization.
- Fully automatic operation & simple maintenance: PLC auto running with touch screen operation, real-time monitoring of running parameters. All maintenance points are centralized for easy inspection.
- Robust container housing for outdoor environment: Anti-corrosion and weatherproof box, works reliably under outdoor, coastal and mining harsh conditions.
- Expandable modular design: Can be matched with pre-treatment units, or combined with secondary RO / EDI / mixed bed system to build complete water treatment line according to water quality requirements.
- Customized design & stable desalination performance: Membrane type, recovery rate and technical route can be designed individually based on raw water lab report to guarantee stable outlet water quality.
Overseas Engineering Cases
Global Project References of Containerized RO Water Treatment Plant
- Middle East Mining Site Brackish Water Treatment: We supplied 8m³/h container RO systems for remote mining camps. Raw water is high TDS brackish groundwater. The mobile unit provides stable drinking & process water for mine workers. The container design adapts high-temperature desert outdoor environment, no civil construction required.
- Southeast Asia Food Factory Process Water Project: Containerized RO plant for food & beverage production. The system produces low-TDS purified water for beverage blending. Fast installation helped client shorten factory construction schedule, and the fully automatic control reduces local labor operation work.
- Africa Temporary Power Station Boiler Feed Water: 8m³/h container RO equipment used as boiler feed water pretreatment unit. The mobile design allows relocation after power station project completed, improving asset ROI. System runs continuously under dusty remote field conditions.
- South America Industrial Wastewater Reuse Project: Container RO system for factory circulating water reuse. The equipment treats industrial wastewater and reuses permeate for production cleaning, helping customer cut freshwater consumption and meet local environmental discharge regulations.
- Ocean Coastal Construction Camp Emergency Water Supply: Containerized desalination RO unit for coastal construction project. Anti-corrosion container and 316SS optional fittings resist salt fog, providing reliable fresh water for offshore engineering teams.
All these overseas projects adopt our containerized RO solution. We can adjust configuration according to local raw water, voltage, climate and environmental regulations. We have exported complete water treatment equipment to more than 30 countries across Asia, Africa, Middle East and Latin America.
Customized Service
Tailor-Made Water Treatment Solution For Your Project
As a 20-year professional water treatment manufacturer, we provide full-set customized service for containerized reverse osmosis systems, not limited to standard 8m³/h model.
- Raw Water Targeted Design: Send your raw water test report, our engineering team will calculate TDS, hardness, turbidity and other indicators, select matching membrane, pump and pretreatment modules, confirm system recovery rate and stable effluent index.
- Material Customization: Optional 304 stainless steel / 316 stainless steel pipeline and frame for coastal, high-corrosion, chemical industry scenarios. Anti-salt-fog, thermal insulation container modification available for extreme temperature zones.
- Capacity Customization: Container RO system range from 500L/H up to 60m³/h, we can design 20GP / 40GP container size according to your required flow rate.
- Post-process Matching Customization: Can add secondary RO, EDI, mixed bed, UV sterilizer, ozone disinfection after main RO system, to reach ultra-pure water standard for electronics, pharmaceutical industry.
- Power & Electrical Customization: Support different industrial voltage & frequency (380V/415V/480V, 50Hz /60Hz) to match global country power grid. Multi-language PLC touch screen optional.
- Packing & Export Service: Professional export packaging, complete documents for customs clearance. We also provide overseas technical guidance, remote commissioning and spare parts supply.
Our engineers will make CAD layout drawing, process flow diagram and equipment quotation for you after confirming your water demand.
About Our Company
We are an original factory with 20 years of professional experience in manufacturing water treatment equipment. We focus on R&D and production of reverse osmosis, ultra-pure water, brackish water desalination, seawater desalination, two-stage RO + EDI + mixed bed systems. Our product range covers capacity from 500L/H up to 60T/H, with rich experience in overseas engineering and export business.
With 20 years of technology accumulation, we master membrane system design, pipeline layout and PLC programming. We are capable to solve complex on-site water treatment problems.
As direct manufacturer, we carry out independent production and strict quality inspection. Pressure test and whole-system commissioning are finished before delivery, so the machine can produce qualified water once delivered, cutting intermediate costs.
We provide custom containerized solution service. We adjust container size, process configuration based on raw water TDS, required water output and site limitation.
We have long-term export experience, familiar with overseas power standard, different raw water characteristics and international working conditions. We can provide matched configuration and export technical support for global projects.
We offer full-cycle service: raw water quality testing, proposal design, production, assembly, on-site commissioning and after-sales technical support, forming a complete service system for customers.


