



| Quantity: | |
|---|---|


KY-RO1000L/H
KAIYUAN
Product Description
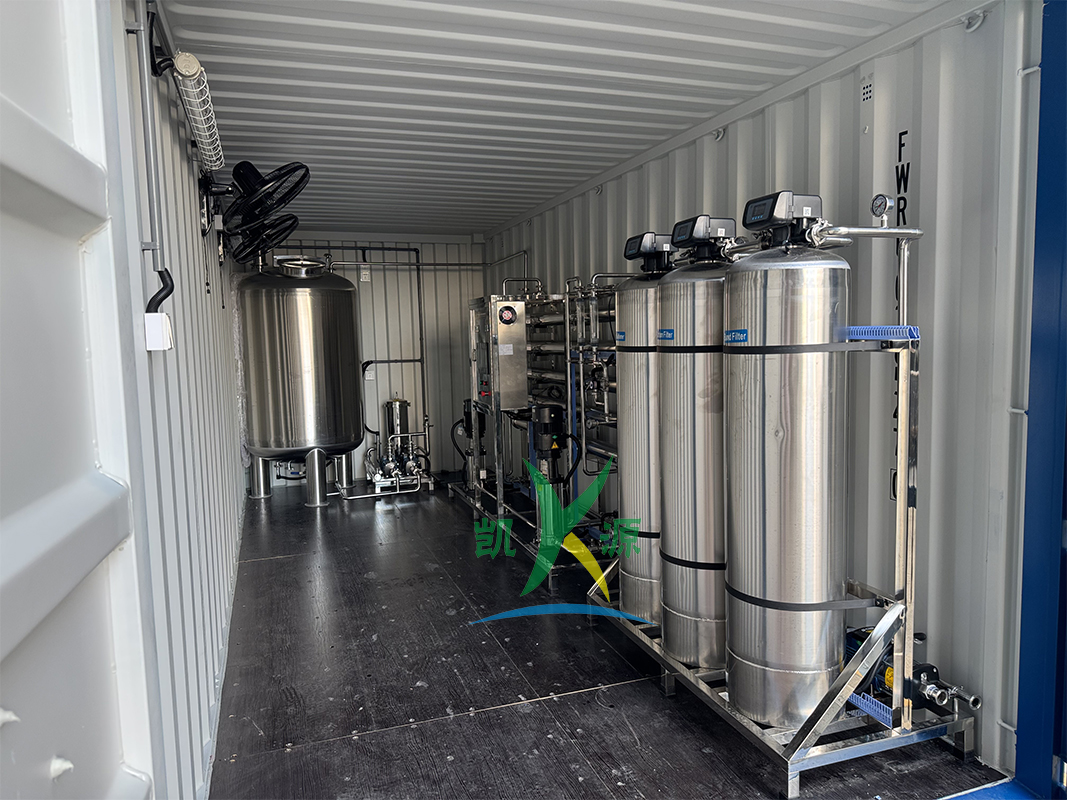
This containerized two-stage reverse osmosis system features a rated water output of 1000 liters per hour. The complete water purification process is pre-installed inside a standard shipping container as an integrated skid-mounted water purification unit. All pipelines, pressure vessels, water tanks and frames in direct contact with water are manufactured from food-grade stainless steel. Adopting double-stage RO purification technology, it achieves step-by-step water polishing. Raw water first passes through the first-stage RO unit to remove most dissolved solids, colloids, suspended solids, heavy metal ions, bacteria and organic contaminants. The pre-purified water then flows into the second-stage polishing RO module to further reduce residual ions, consistently producing purified water that meets strict standards for industrial, medical, food and laboratory applications.
Different from conventional site-assembled reverse osmosis machines, this containerized unit is fully pre-plumbed, pre-wired, pre-programmed, pressure-tested and water-tested before delivery. Once delivered to your site, you only need to connect raw water inlet, power supply and concentrated water discharge pipe to start production. It eliminates the long cycle of building dedicated water treatment rooms, on-site assembly and complicated commissioning. The system works well with tap water, groundwater and surface water. It delivers stable high-purity purified water continuously, widely used for bottled water production, food processing, hemodialysis water supply, university & enterprise laboratories and precision reagent preparation scenarios requiring stringent water quality.
The core advantage of two-stage RO is stable desalination performance. It maintains steady TDS and resistivity even when raw water TDS fluctuates with seasonal changes. The full stainless steel flow path avoids impurity leaching and biofilm growth issues of ordinary PVC pipes, complying with sanitary water standards. The container shell provides windproof, rainproof, dustproof and temperature-resistance protection. It can be placed indoors or outdoors, ideal for sites with limited space, temporary projects, relocating factories and standardized chain production lines. Combining automatic operation, low maintenance and mobile flexibility, it is a modular premium choice for high-purity water production.
Single-stage RO only provides basic desalination and leaves trace soluble ions, which cannot meet strict requirements for dialysis and laboratory water. This system adopts series two-stage RO design. The first RO removes more than 98% TDS, colloids, bacteria and macromolecular organics. The second polishing RO further captures residual salts and micro contaminants. The overall desalination rate is greatly improved with minimal water quality fluctuation, solving the common problem of unstable outlet water from single-stage RO systems.
All pre-treatment filters, high-pressure pumps, RO membrane housings, membrane elements, intermediate tanks, control panels and sampling assemblies are integrated inside the standard container. Full factory commissioning is completed before shipment. No complicated on-site assembly, welding or pipe fitting work. Traditional water treatment projects take weeks from construction to first water production. This container RO unit can be put into service shortly after pipe connection, greatly shortening project lead time. Perfect for urgent projects, temporary water supply, overseas projects and decentralized water stations.
All wetted parts use premium stainless steel instead of FRP or plastic pipes. Smooth stainless steel inner surface resists scaling and biofilm adhesion, easy for CIP cleaning. No plasticizer leaching, fully compliant with food and medical sanitary regulations. It tolerates acid and alkaline cleaning chemicals, less damage during routine chemical cleaning. Great corrosion resistance for humid water treatment environments, longer service life and lower long-term depreciation cost.
Equipped with PLC control system, online TDS monitor, flow sensors, pressure transmitters and multi-level safety protection. The system automatically stabilizes inlet pressure, produces purified water, drains concentrate water and flushes RO membranes periodically. It has low-pressure protection, over-pressure protection, motor overload protection and audible & visual fault alarm. Operators can check real-time water quality, flow and pressure on the touch screen without constant on-site attendance. It reserves signal interfaces for central SCADA monitoring to cut factory labor cost. Simple training is enough for daily inspection.
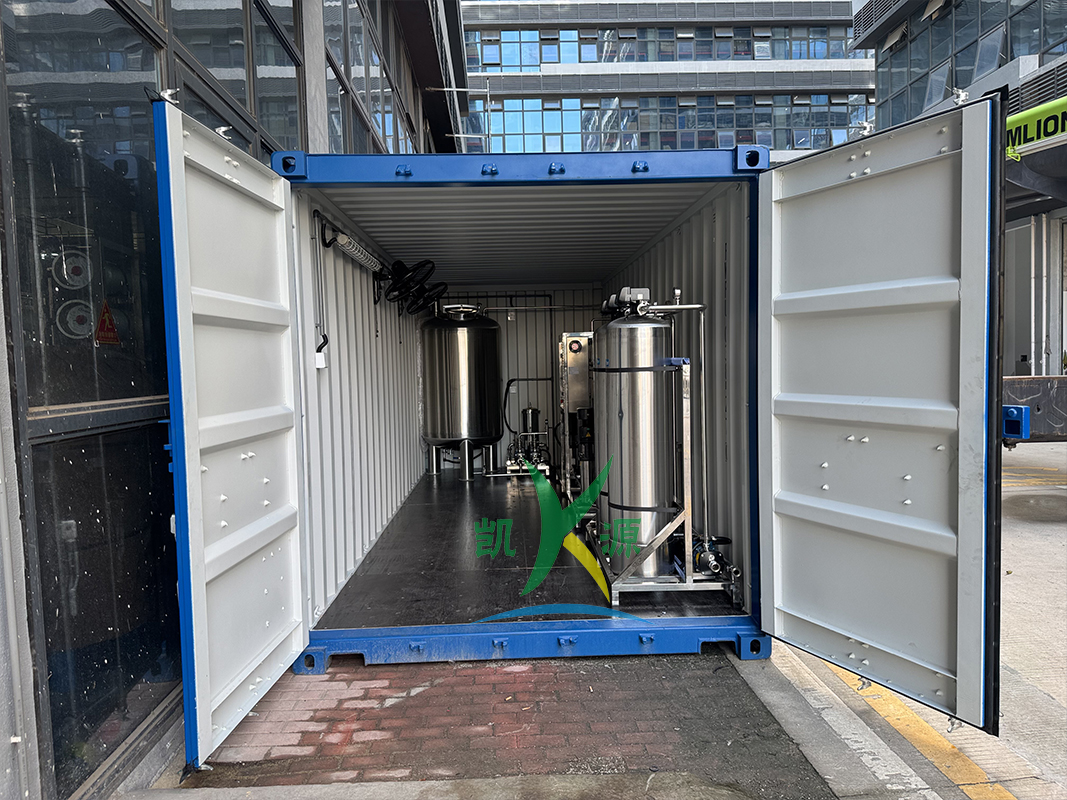
Built in standard shipping container, the whole unit can be lifted, transported by truck or sea freight. When factories relocate or temporary projects finish, the complete system can be hoisted and moved to a new site for reuse, improving asset utilization. The modular design supports later upgrades. You can add UV sterilizer, EDI module or polishing mixed bed to upgrade to ultra-pure water system based on future water demand.
Fitted with energy-saving high-pressure RO pumps. Hydraulic layout optimized by fluid simulation to reduce pipe friction loss, controlling power consumption per ton of water while keeping proper membrane working pressure. Concentrate water recycling port is reserved. You can return concentrate water back to pre-treatment to boost water recovery rate, save water cost and comply with water-saving environmental policies.
Full workflow: Raw water boosting → Pre-treatment (Multi-media filter + Activated carbon filter + Cartridge filter) → 1st stage high pressure pump → 1st RO membrane assembly → Intermediate tank → 2nd stage high pressure pump → 2nd polishing RO → Purified water outlet. Independent pressure gauge, flow meter and sampling port for each RO stage, convenient for segmented water quality testing and fast troubleshooting. Anti-fouling RO membranes with high flux, stable rejection rate and good tolerance to regular chemical cleaning to prevent performance decay.
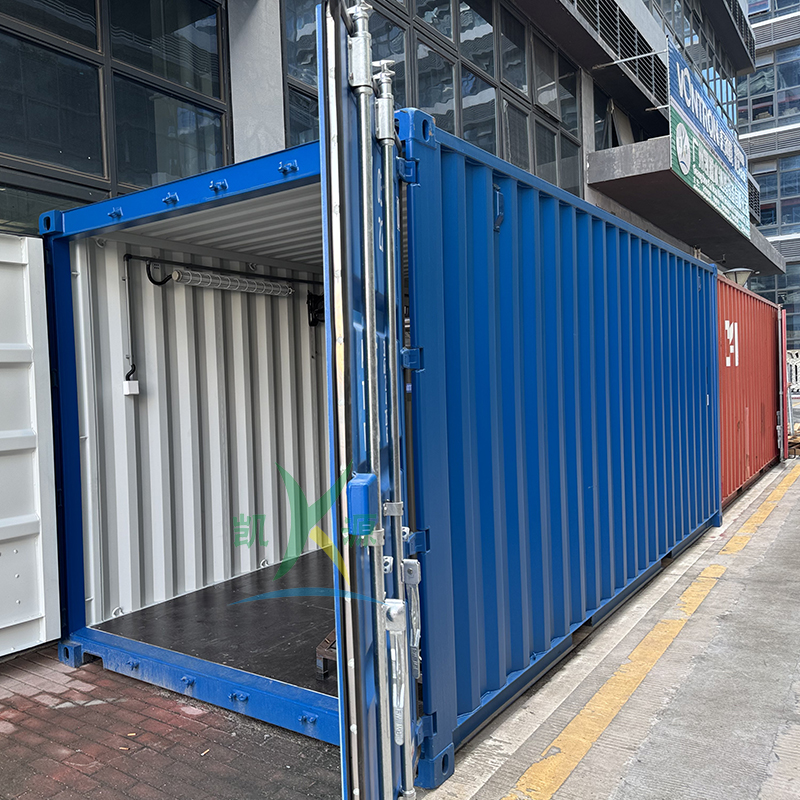
Frame, membrane housings, water tanks, valves and pipelines are stainless steel with polished surface. Outer shell is standard shipping container with double opening doors to reserve enough maintenance space. Internal lighting and ventilation system are installed for filter replacement and membrane service. The container structure is sturdy, anti-collision, rainproof and heat insulated for outdoor installation. All seals are food-grade aging-resistant rubber to avoid secondary pollution.
PLC touch screen control with intuitive interface. Online TDS probes monitor product water TDS of first stage and final polished water. Equipped with raw water pressure gauge, pump outlet gauge, membrane inlet/outlet gauge, product water flow meter and concentrate flow meter. Automatic membrane flushing runs when the system shuts down to wash away surface contaminants and reduce scaling, extending membrane lifespan. Fault codes pop up automatically for fast maintenance.
Multi-layer safety protection: low inlet pressure protection to avoid dry pump running, over-pressure protection to prevent membrane damage, tank level interlock, motor overload protection and electric leakage protection. Electric cabinet is separated far from humid areas to meet industrial electrical standards. Pressure relief valves are installed for safe pressure release before maintenance.
Maintenance aisles reserved inside the container. Valves and filters are arranged ergonomically for easy cartridge and membrane replacement. Independent sampling valves for anytime water testing. Clear labels for product water, concentrate water and drain ports to avoid wrong connection. Waterproof cable trunking for neat wiring. Operation manual, tutorial video and spare parts list are supplied for easy operation.
Purified water and mineral water bottling, juice, tea drink, dairy and seasoning production. Water quality directly affects product taste, shelf life and food safety. Stainless steel two-stage RO reliably removes heavy metals, bacteria and residual chlorine, prevents scaling and odor. It meets food sanitation standards, suitable for new or upgraded water supply systems for small & medium beverage factories and water plants.
Hemodialysis centers and hospital dialysis rooms. Dialysis water has strict limits on bacteria, endotoxin and ion content. Two-stage RO reduces ion concentration steadily, lowering the load of dialysis machines and reducing patient complication risks. Containerized design is ideal for new dialysis centers, township hospitals and temporary dialysis stations without dedicated water treatment rooms.
University labs, third-party testing labs, pharmaceutical R&D laboratories and analytical chemistry labs. Chemical testing, chromatography, reagent preparation, cell culture and sample dilution require low-ion pure water. This 1000L/H two-stage RO unit provides stable central pure water supply. You can add ultra-pure water cartridges to get Grade 1 / Grade 2 lab water, solving the capacity bottleneck of small bench-top water purifiers.
It also works for cosmetic batching, fine chemical mixing, battery production, boiler make-up water and plant tissue culture water. For remote camps, islands and mining sites without dedicated water workshops, this container RO plant independently produces qualified process water.
The containerized unit fits global logistics systems perfectly. It can be transported by flatbed truck, barge or ocean container shipping without extra custom frames. All pipelines, gauges and membranes are fixed with shockproof protection before shipment. Fragile sensors are protected to avoid damage during transit. The container can be locked to stop dust and rain during transportation.
Standard lifting points are used for hoisting, compatible with common cranes at ports and construction sites. Only flat hardened ground with sufficient bearing capacity is required for placement, no special waterproof or anti-corrosion room construction needed. On-site installation steps are simple: connect raw water pipe, 380V industrial power supply, concentrate drain pipe and purified water delivery pipe. Check valve status and start the system on touch screen after parameter confirmation.
For overseas export orders, we provide export packaging, customs documents and CE / ISO supporting certificates. If inland transportation is restricted at destination, we can disassemble non-core components for separate shipment and guide reassembly. We offer remote commissioning guidance, and on-site engineer training is available upon request. The mobility advantage cannot be matched by fixed room-based RO systems, the whole unit can be lifted and reused for new projects after the old project ends.
Rated Output: 1000 L/H (25℃ standard temperature, final two-stage RO water)
Process: Two-Stage Reverse Osmosis, Sanitary Stainless Steel Piping
Container Size: Standard 20GP (Custom size available)
Inlet Water Source: Tap water, Groundwater, Surface water (Recommended TDS ≤1000ppm)
Power Supply: 380V / 50Hz 3-phase (60Hz & special voltage customizable)
Control Mode: PLC + Touch Screen Automatic Control, Online TDS Monitoring, Auto Flush, Fault Alarm
Wetted Material: SS304 Stainless Steel (Upgrade to SS316L for higher anti-corrosion demand)
Membrane Type: Anti-fouling Polyamide RO Membrane
Desalination Rate: 1st stage ≥98%, Overall two-stage ≥99.2%
Operation Mode: 24h continuous running, intermittent start-stop supported
Optional Accessories: UV Sterilizer, EDI Module, Ozone Sterilizer, Remote Data Transmission Module
Working Environment: Indoor / Outdoor, Ambient Temp 5~45℃
Total Weight: About 8.5 Tons (without external piping)
Our old single-stage RO often had TDS out of range in rainy seasons with unstable water taste. After switching to this container two-stage RO, water quality stays consistent. Stainless steel pipes are easy to clean. We put it on our empty yard without building a dedicated room, saving huge construction cost. It runs right after connecting water and power. Our engineer support is responsive, daily maintenance workload is much lower and the capacity matches our filling line perfectly.
Our new dialysis building has limited space and no spare room for water treatment. We chose this container two-stage RO. Outlet water meets dialysis water standards. Online water monitor lets nurses check water quality anytime, and fault alarm makes us feel safe. We can relocate the whole unit if the hospital moves, great value for long-term investment.
Our bench-top water purifiers could not meet daily pure water demand for testing. This 1000L/H container RO provides stable water supply with low quality variation, which improves test repeatability. We added UV sterilizer later inside the container to control microbes. Fully automatic, no full-time operator required.
Local technicians cannot assemble water treatment systems on site. This pre-commissioned container RO was shipped to our port, and started working after simple pipe connection. Stainless steel resists coastal humid salt environment, no pipe corrosion after more than one year running.
Every container two-stage RO unit passes strict pressure test and water trial run before delivery. We provide warranty service, free repair and replacement of core parts for non-human damage during warranty period. Complete technical documents are supplied: General layout drawing, P&ID diagram, electrical schematic, operation manual and membrane maintenance guide. Original spare parts including RO membranes, filter cartridges, O-rings and cleaning chemicals are available long-term. Lifetime technical support is provided for troubleshooting, membrane CIP guidance and water quality optimization. Custom capacity, container size, material upgrade and post-treatment modules are available to build exclusive purified water solutions.


